Medical Equipment Manufacturers: Understanding Production Standards And Regulatory Compliance

Manufacturing processes, supply chain oversight, and testing protocols in device production
Manufacturing processes for medical devices can vary from manual assembly to highly automated lines, depending on device complexity and production volume. Process qualification activities—such as equipment installation qualification (IQ), operational qualification (OQ), and performance qualification (PQ)—may be used to document that equipment and processes perform consistently. Environmental controls for cleanrooms, laminar flow zones, or controlled storage are often specified when devices are sensitive to particulate or microbial contamination, and monitoring data may be retained as part of release documentation.
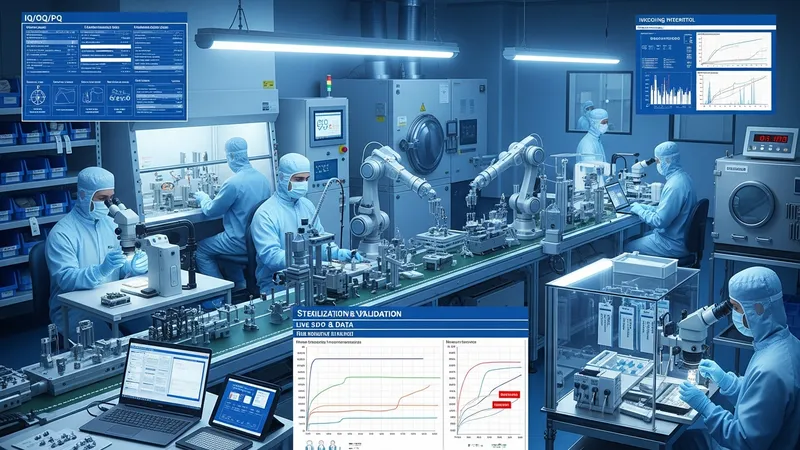
Component inspection and in-process controls typically support consistent quality. Incoming inspection criteria, in-process sampling plans, and final release tests can be defined based on device risk and criticality of components. Statistical process control methods may be used to monitor key parameters and identify trends before they lead to out-of-specification product. For devices requiring sterilization, validation protocols for sterilization cycles and sterility assurance level targets are commonly documented, and packaging integrity tests may be performed to confirm barrier performance.
Supply chain resilience and traceability are often areas of regulatory focus. Manufacturers may maintain bills of materials that list approved suppliers and part numbers, and they may require suppliers to notify them of changes that could affect performance. Where single-source components are used, contingency planning and alternative qualified suppliers are considered as risk mitigations. Batch or lot tracking systems can facilitate recalls or targeted communications if a distributed component is later found to be nonconforming.
Testing protocols are commonly tailored to the device’s intended function and applicable standards. Bench testing may cover mechanical durability, electromagnetic compatibility, or software performance, while biocompatibility assessments may be necessary for devices with tissue contact. Manufacturers often compile test reports and certificates from accredited laboratories to support technical documentation. These results may be used for internal release decisions and to satisfy external conformity assessments as required by regulators or standards bodies.